How Chemical Manufacturing Companies Are Revolutionizing Industries

Chemical manufacturing companies are at the forefront of innovation, reshaping industries by delivering cutting-edge solutions that enhance efficiency and sustainability.
How Chemical Manufacturing Companies Are Revolutionizing Industries
Chemical manufacturing companies are at the forefront of innovation, reshaping industries by delivering cutting-edge solutions that enhance efficiency and sustainability. From developing advanced materials to pioneering sustainable practices, these companies are playing a pivotal role in transforming various sectors. This article delves into the multifaceted contributions of chemical manufacturing companies, examining their impact on different industries, sustainable practices, advancements in technologies, and future trends.
The Role of Innovation in Chemical Manufacturing
Innovation is the lifeblood of the chemical manufacturing industry. It drives the development of new products, processes, and technologies that meet the evolving needs of various markets. One of the most significant innovations in this field is the development of advanced materials such as high-performance polymers, nanomaterials, and composites. These materials have revolutionized industries like aerospace, automotive, and electronics by offering superior properties such as increased strength, lighter weight, and enhanced durability.
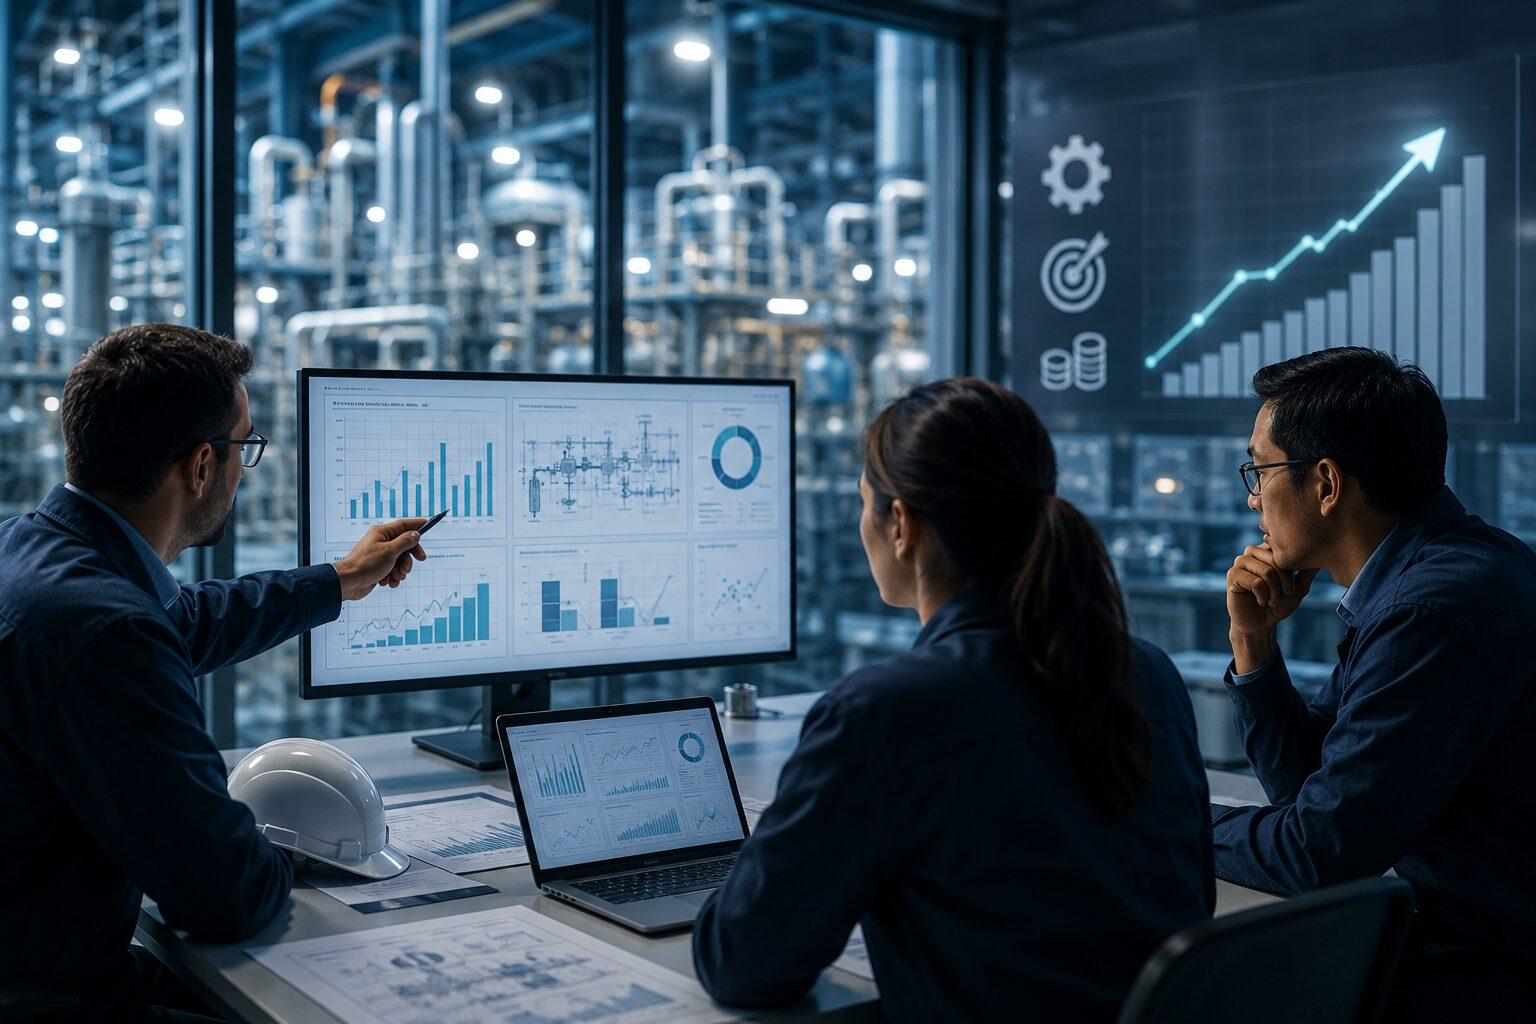
Moreover, innovation in chemical manufacturing extends to process optimization. Advanced process technologies such as continuous manufacturing, process intensification, and digitalization have significantly improved production efficiency. Continuous manufacturing, for instance, allows for the uninterrupted production of chemicals, reducing downtime and increasing output. Digitalization, on the other hand, enables real-time monitoring and control of manufacturing processes, leading to better quality control and reduced waste.
Innovation is also driving the development of greener and more sustainable chemicals. Companies are increasingly focusing on creating bio-based chemicals and materials that reduce reliance on fossil fuels. For example, bio-based plastics derived from renewable resources like corn and sugarcane are gaining popularity as environmentally friendly alternatives to traditional plastics. These innovations are not only transforming industries but also contributing to a more sustainable future.
Sustainable Practices in Chemical Manufacturing
Sustainability has become a key focus for chemical manufacturing companies, driven by the growing awareness of environmental issues and the need for responsible business practices. One of the primary ways chemical manufacturers are promoting sustainability is through the adoption of green chemistry principles. Green chemistry focuses on designing products and processes that minimize the use and generation of hazardous substances. This approach not only reduces the environmental impact of chemical manufacturing but also enhances the safety of workers and consumers.
Energy efficiency is another critical aspect of sustainability in chemical manufacturing. Companies are investing in energy-efficient technologies and processes to reduce their carbon footprint. For example, the use of advanced catalysts in chemical reactions can lower energy consumption and increase reaction efficiency. Additionally, chemical manufacturers are exploring renewable energy sources such as solar and wind power to meet their energy needs, further reducing their reliance on fossil fuels.
Waste reduction and recycling are also integral to sustainable practices in chemical manufacturing. Companies are implementing closed-loop systems that allow for the recycling and reuse of chemicals and materials. By recovering valuable by-products and minimizing waste generation, chemical manufacturers can reduce their environmental impact and improve resource efficiency. Furthermore, the development of biodegradable and recyclable materials is helping to address the global issue of plastic waste.
Advancements in Chemical Processing Technologies
Technological advancements in chemical processing are revolutionizing the way chemicals are manufactured. One of the most significant advancements is the development of continuous processing technologies. Unlike traditional batch processing, continuous processing allows for the uninterrupted production of chemicals, leading to increased efficiency and reduced production costs. This technology is particularly beneficial for large-scale production and has been widely adopted in the pharmaceutical and petrochemical industries.
Process intensification is another area where significant advancements have been made. This approach involves redesigning chemical processes to make them more efficient and compact. By integrating multiple process steps into a single unit, process intensification can reduce the size of manufacturing plants, lower energy consumption, and increase production rates. Microreactors, which are small-scale reactors that enable precise control of chemical reactions, are a prime example of process intensification technology.
The integration of digital technologies, such as the Internet of Things (IoT), artificial intelligence (AI), and machine learning, is also transforming chemical processing. These technologies enable real-time monitoring and control of manufacturing processes, leading to improved process optimization and quality control. For instance, predictive maintenance powered by AI can identify potential equipment failures before they occur, reducing downtime and maintenance costs. Furthermore, digital twins—virtual replicas of physical assets—allow for the simulation and optimization of chemical processes, enhancing overall efficiency.
The Impact of Chemical Manufacturing on Supply Chains
Chemical manufacturing plays a crucial role in global supply chains, providing essential raw materials and intermediates for various industries. The reliability and efficiency of chemical supply chains are vital for the seamless operation of downstream industries such as pharmaceuticals, automotive, and consumer goods. Any disruption in the supply of chemicals can have a ripple effect, impacting production and distribution across multiple sectors.
One of the ways chemical manufacturers are strengthening supply chains is through the adoption of digital supply chain technologies. These technologies enable real-time visibility and tracking of chemical shipments, ensuring timely delivery and reducing the risk of supply chain disruptions. Advanced analytics and AI can also be used to optimize inventory management, demand forecasting, and supply chain planning, enhancing overall efficiency.
Sustainability in supply chains is another critical focus for chemical manufacturing companies. By implementing sustainable sourcing practices, companies can ensure that the raw materials they use are sourced responsibly and ethically. This includes partnering with suppliers who adhere to environmental and social standards and investing in traceability systems to track the origin of raw materials. Additionally, chemical manufacturers are exploring circular economy models, where materials are recycled and reused within the supply chain, reducing waste and conserving resources.
Future Trends in Chemical Manufacturing
The future of chemical manufacturing is poised to be shaped by several key trends. One of the most significant trends is the increasing focus on sustainability. As environmental concerns continue to rise, chemical manufacturers are expected to adopt more sustainable practices and develop greener products. This includes a shift towards bio-based chemicals, renewable energy, and circular economy models. Companies that prioritize sustainability will likely gain a competitive edge in the market.
Digital transformation is another trend that will continue to drive the industry forward. The integration of digital technologies such as IoT, AI, and blockchain will enhance process optimization, supply chain management, and product development. Predictive analytics and machine learning will enable companies to make data-driven decisions, improving efficiency and reducing costs. Additionally, digitalization will facilitate greater collaboration and transparency across the chemical manufacturing value chain.
Innovation in materials science is expected to lead to the development of next-generation materials with enhanced properties and functionalities. These advanced materials will have applications across various industries, from healthcare to electronics to energy. For example, the development of smart materials that can respond to external stimuli, such as temperature or pressure, will open up new possibilities for product design and performance. The continued exploration of nanotechnology and biotechnology will also contribute to the creation of novel materials and solutions.
Conclusion: The Ongoing Revolution in Chemical Manufacturing
The chemical manufacturing industry is undergoing a profound transformation, driven by innovation, sustainability, and technological advancements. Chemical manufacturers are at the forefront of developing new materials, optimizing processes, and implementing sustainable practices that are reshaping industries and addressing global challenges. From healthcare to automotive to agriculture, the impact of chemical manufacturing is far-reaching and transformative.
As the industry continues to evolve, the focus on sustainability and digitalization will be paramount. Companies that embrace these trends and invest in research and development will be well-positioned to lead the ongoing revolution in chemical manufacturing. The development of greener products, energy-efficient processes, and advanced materials will not only enhance industry competitiveness but also contribute to a more sustainable and resilient future.
The journey of chemical manufacturing is one of continuous innovation and adaptation. While challenges remain, the potential for growth and impact is immense. By leveraging cutting-edge technologies and sustainable practices, chemical manufacturing companies will continue to revolutionize industries and shape a better world for future generations.
Want more insights like this?
Sign up for our newsletter and be the first to get the goods. Dive deeper into the world of chemical innovation and industry trends by signing up for our newsletter today!
Ready to Get Started?
Value-focused customization is at the core of what we do. Our custom-engineered chemicals are tailored to the unique needs of each facility and process. This high level of customization allows Americo products to consistently outperform generic solutions from leading competitors.